GMI paper packaging must meet requirements for print quality, color consistency, and product identification. These factors help businesses maintain a consistent brand image and satisfy the standards of domestic and international partners.
Choosing a qualified printing GMI packaging manufacturer is an important step in securing reliable production quality. In this article, Khang Thanh presents the key criteria for evaluating a supplier, including certification, printing capabilities, and quality control processes.
The importance of evaluating GMI packaging suppliers before ordering
Many businesses assume that choosing a printer with GMI certification automatically guarantees high-quality packaging. In reality, without carefully assessing the supplier’s manufacturing capabilities and quality control system, companies may still face several risks, including:
- Inconsistent brand colors: Colors differ from brand guidelines or vary between production batches.
- Unreliable barcodes and QR codes: Codes become difficult or impossible to scan, affecting inventory management and product distribution.
- Export shipment rejection: GMI paper packaging fails to meet the quality requirements of global brands or international retailers.
- Batch-to-batch inconsistency: Variations in color, graphics, and print quality across different production runs.
- Higher operational costs: Additional expenses from reprinting, delayed deliveries, customer complaints, or contractual penalties.
Understanding these evaluation criteria from the beginning helps businesses select a reliable printing GMI paper packaging supplier, reduce production risks, and maintain consistent packaging quality over time.
>>> Understanding GMI packaged products | GMI certification for packaging quality
7 key factors for assessing a GMI paper packaging manufacturer
Besides requesting proof of GMI certification, what other factors should businesses consider when evaluating a supplier of GMI paper packaging?
Brand color accuracy and consistency
Color consistency is the most critical requirement of the GMI standard. Therefore, GMI packaged products must accurately reproduce the brand’s approved colors while maintaining consistency across every production run.
Color deviations can lead to rejected shipments, particularly for international brands with strict color compliance requirements.
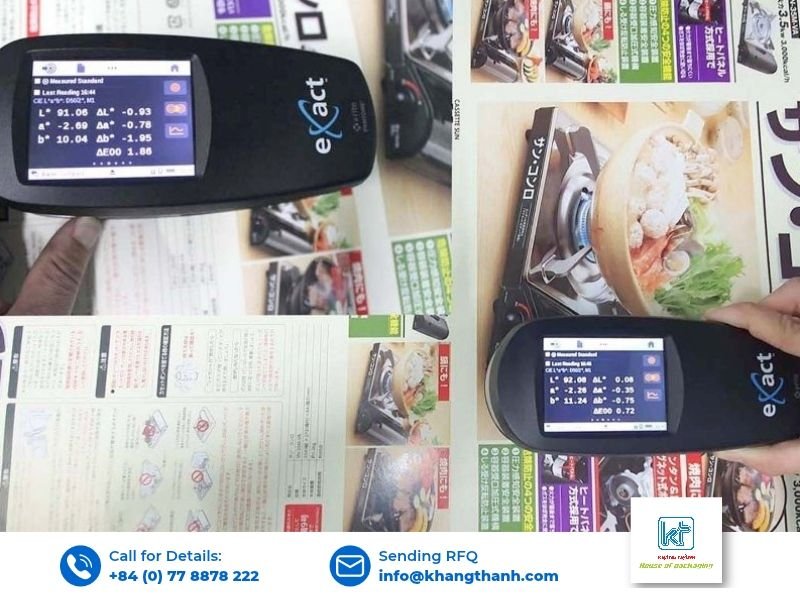
For that reason, brands should request physical print samples or review previously completed production batches, then compare against official color (Pantone, brand color specifications). In addition, suppliers should be able to provide instrument-based color measurement reports instead of relying solely on visual inspection.
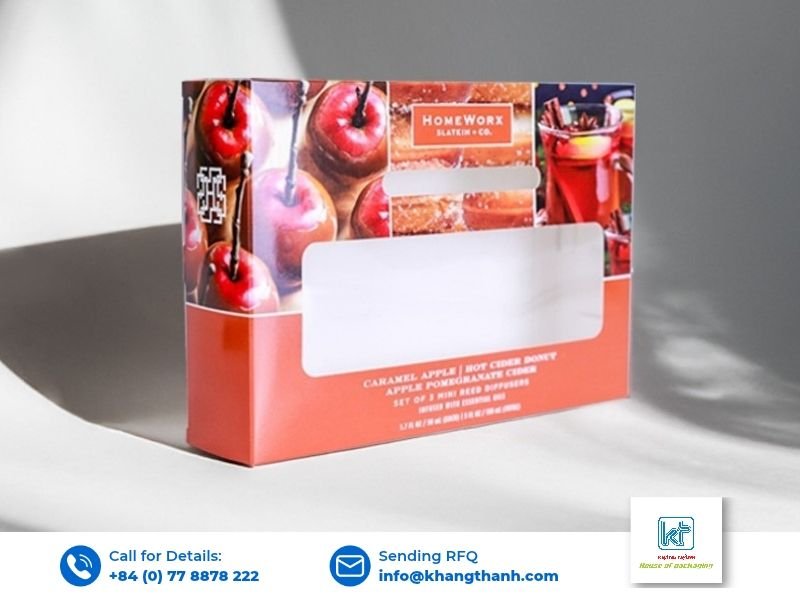
Image reproduction and text legibility
Beyond color accuracy, image quality directly reflects the capabilities of a printing GMI paper packaging supplier.
In other words, logos, icons, illustrations, and product information should be reproduced with sharp detail, free from ink smudging, missing elements, or jagged edges. Likewise, printed text must remain crisp, legible, and faithful to the original design specifications.
Barcode and QR code scanning reliability
Barcodes and QR codes are essential for warehouse management, product traceability, and retail operations. Therefore, GMI packaged products must feature codes printed with appropriate contrast, precise dimensions, and sufficient print quality to ensure reliable scanning using industry-standard devices.
To verify performance, brands should inspect barcode quality during the proofing stage and approve printed samples before mass production begins.
>>> 5 Tips to optimize rigid boxes wholesale printing costs effectively
Print consistency across production batches
For export-oriented brands, maintaining consistent print quality between production runs is essential. Moreover, it is also one of the key performance indicators assessed under the GMI standard.
When evaluating a supplier, businesses should review recently completed GMI packaged products to determine whether print quality, finishing, and color consistency have been maintained across multiple production batches.
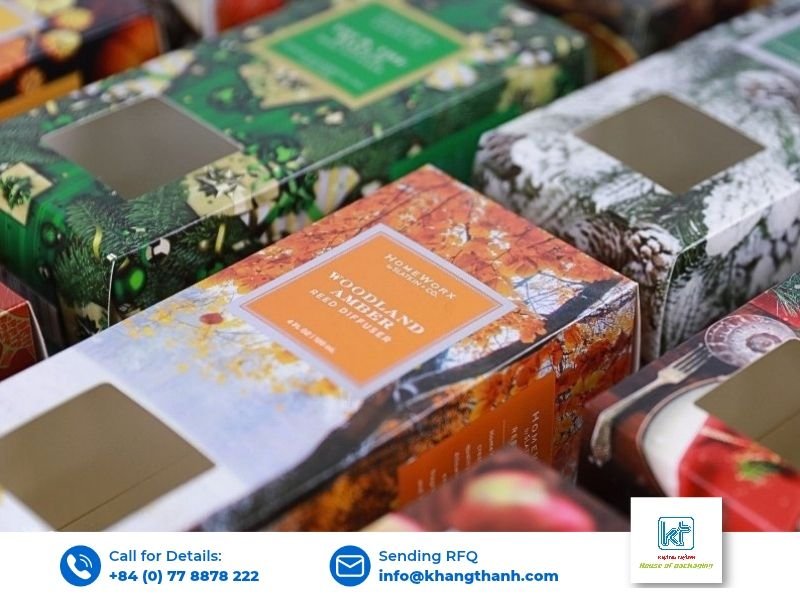
Color control capabilities under the GMI standard
Producing GMI paper packaging requires a standardized color management system rather than relying solely on operator experience. Without a structured workflow, print quality can vary depending on production shifts or individual operators, increasing the likelihood of color inconsistencies.
Therefore, businesses should discuss the supplier’s color management process, color measurement equipment, press calibration procedures, and production monitoring methods to evaluate their technical capabilities.
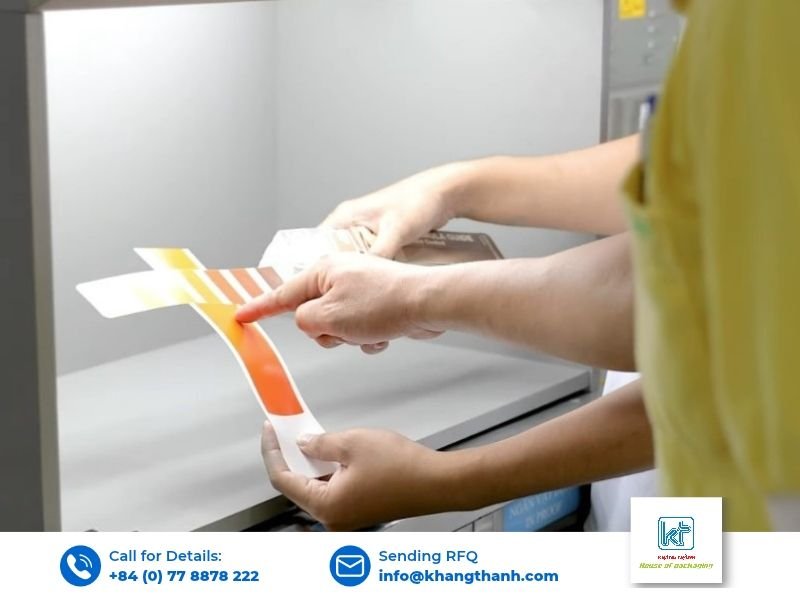
Inspection procedures and quality documentation
Professional suppliers implement quality control throughout the entire production process. This proactive approach helps identify defects early, reducing the likelihood of costly reprints, delayed deliveries, and customer complaints.
Therefore, when selecting a printing GMI packaging provider, customers should prioritize manufacturers with documented quality management procedures, color measurement records, inspection reports, and complete production traceability.
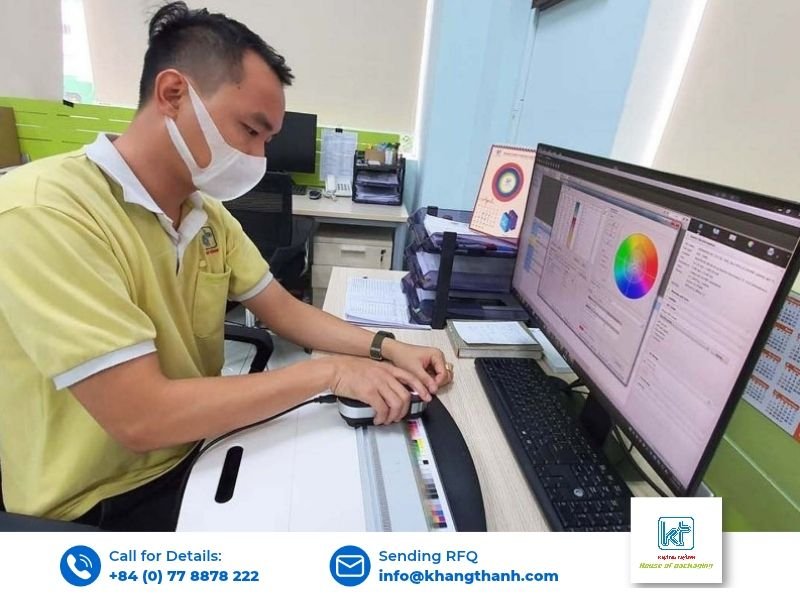
Active GMI certification status
Finally, businesses should verify that the supplier’s GMI certification remains valid and covers the intended production facility.
Some printers previously achieved certification but failed to maintain periodic assessments or allowed their certification to expire. In such cases, their current manufacturing capabilities may no longer comply with the latest GMI standard requirements.
7 factors for selecting the right GMI paper packaging supplier
Since investing in printing GMI paper packaging requires significant resources, businesses should carefully evaluate the following factors before selecting a supplier.
Evaluating supplier GMI level
GMI standard classifies certified printers into different performance levels based on recurring audit results and their ability to maintain consistent print quality. Thus, not every certified printer demonstrates the same level of process control.
There are currently three levels of printing GMI packaging suppliers, the higher the level, the more stable the color management system and production process are.
- Platinum: Outstanding printing performance with continuous scores above 90%.
- Gold & Silver: Strong operational performance with recurring scores between 80% and 89%.
- Bronze: Printers currently under evaluation, typically scoring below 79%.
Check GMI certification coverage at the production facility
Many packaging manufacturers operate multiple factories and production sites. However, GMI standard applies only to the specific facility that has successfully completed the certification audit.
Since certification evaluates machinery, personnel, and production processes at an individual location, businesses should confirm that their GMI paper packaging order will be produced at the certified facility before signing a contract.
Look beyond printing costs to evaluate long-term value
Manufacturers printing GMI paper packaging invest heavily in advanced equipment, color management software, quality control systems, and recurring certification audits. As a result, production costs are often higher than conventional printing services.
However, these investments deliver long-term value through improved print consistency, reduced production risks, and stronger brand protection. By understanding these criteria, brands will gain a better grasp of the sustainability aspects, rather than just the unit cost of GMI packaged products.
Examine the manufacturer’s production capacity and expertise
A qualified GMI packaging supplier should offer more than a valid certificate. In more detail, businesses should also evaluate:
- Modern printing equipment
- Professional color measurement systems
- Standardized quality control procedures
- Experienced technical teams
Whenever possible, schedule a factory visit or request a detailed walkthrough of the supplier’s production process and previous GMI packaged products to gain a more objective assessment.
>>> Khang Thanh achieved 10 international standards in the paper packaging industry
Evaluate actual print quality through pre-production samples
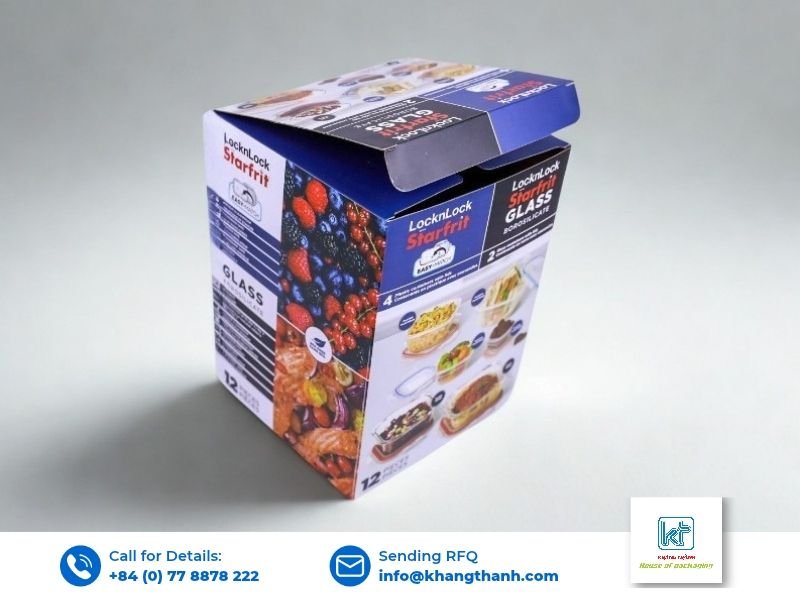
GMI packaging printed proofs serve as the final reference for approving colors, image quality, barcodes, and technical specifications before large-scale production begins.
For this reason, sample approval significantly reduces production errors, provides a physical benchmark for future comparison, and increases accountability throughout the manufacturing process.
Review procedures for handling production issues
Even with experienced suppliers, risks can still occur during the production of bulk GMI packaged products.
Therefore, brands should agree in advance on the error handling process, response time, responsibilities of each party and solutions if the quality of paper packaging does not meet GMI standards as committed. The advantages of this step will help limit unnecessary disputes, build trust and evaluate the responsibility of the packaging supplier.
Using these criteria as a reference allows businesses to make informed decisions when selecting a GMI packaging supplier. This approach helps verify production capabilities, limit printing risks, and maintain uniform quality across all production batches.
Khang Thanh offers tailored GMI certification solutions to meet the expectations of global brands. Contact our packaging specialists to discuss your requirements and identify the right solution for your GMI paper packaging project.
BOXES VIETNAM
Tel: (+84) 77 8878 222
Email: info@khangthanh.com